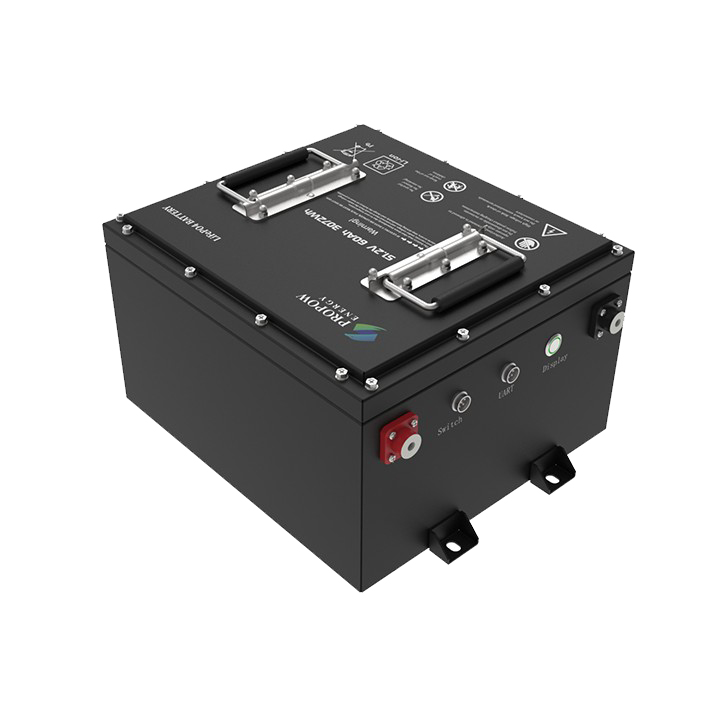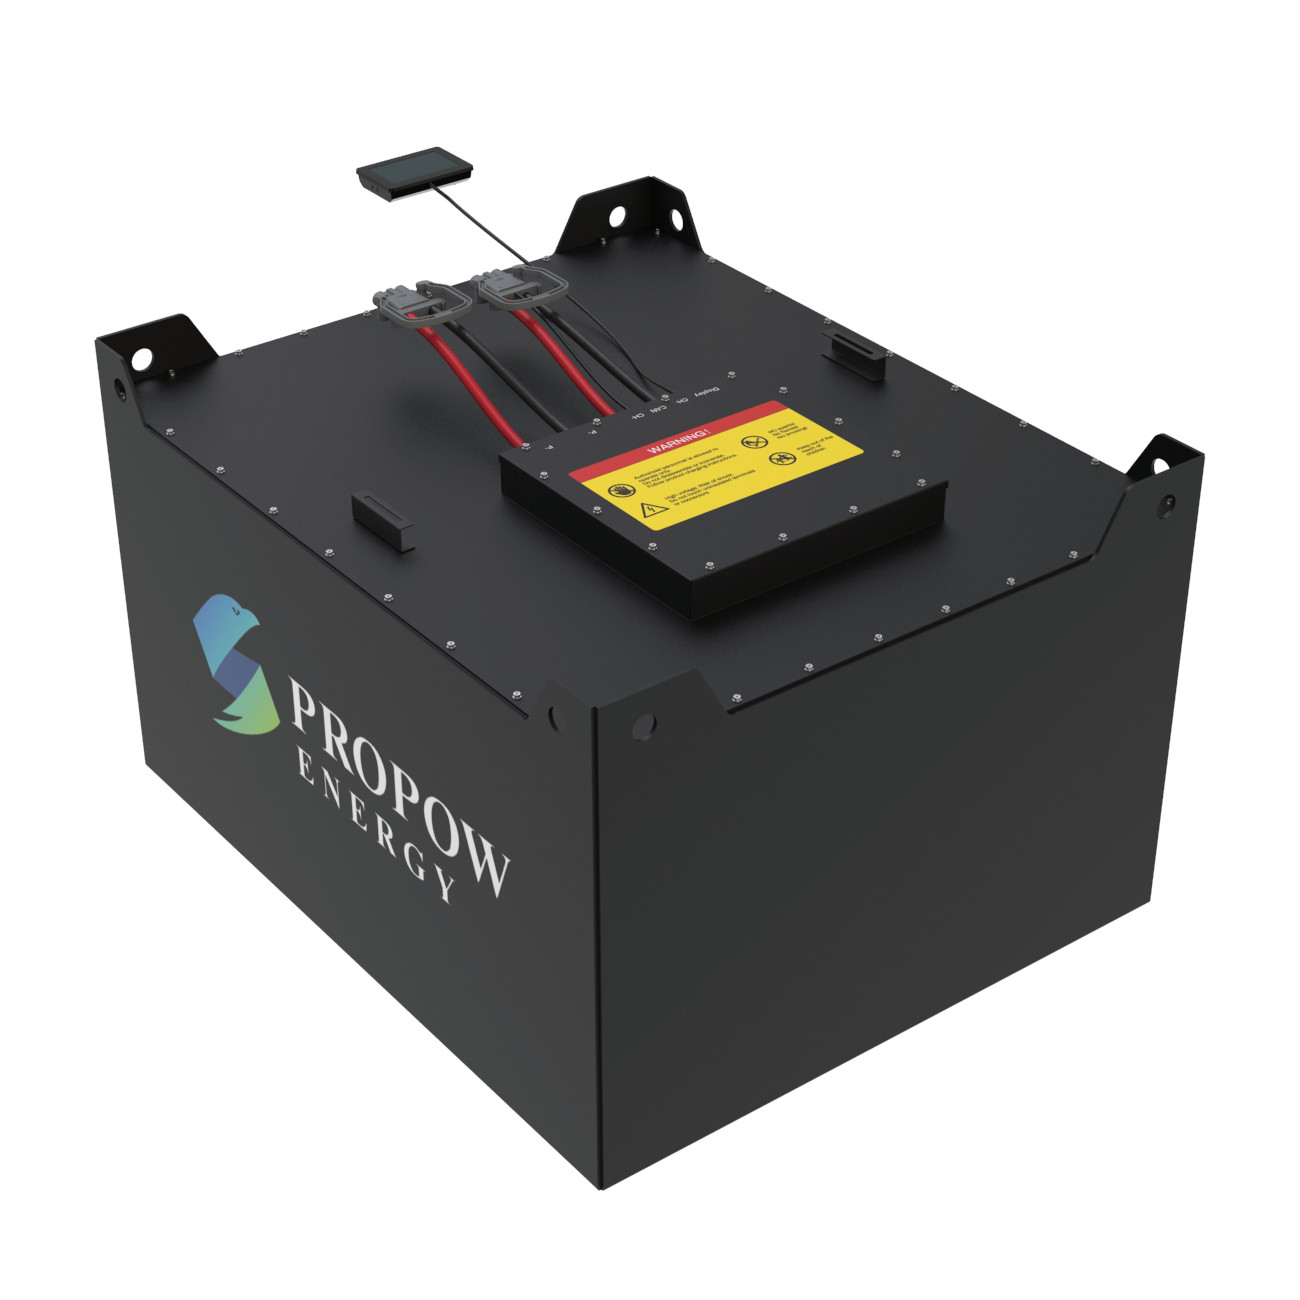
 Forklift LiFePO4 Batteries
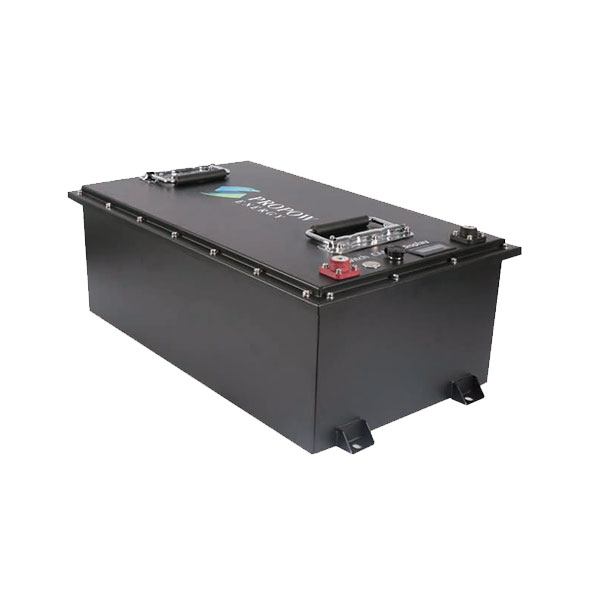 Floor Cleaning Machine Batteries
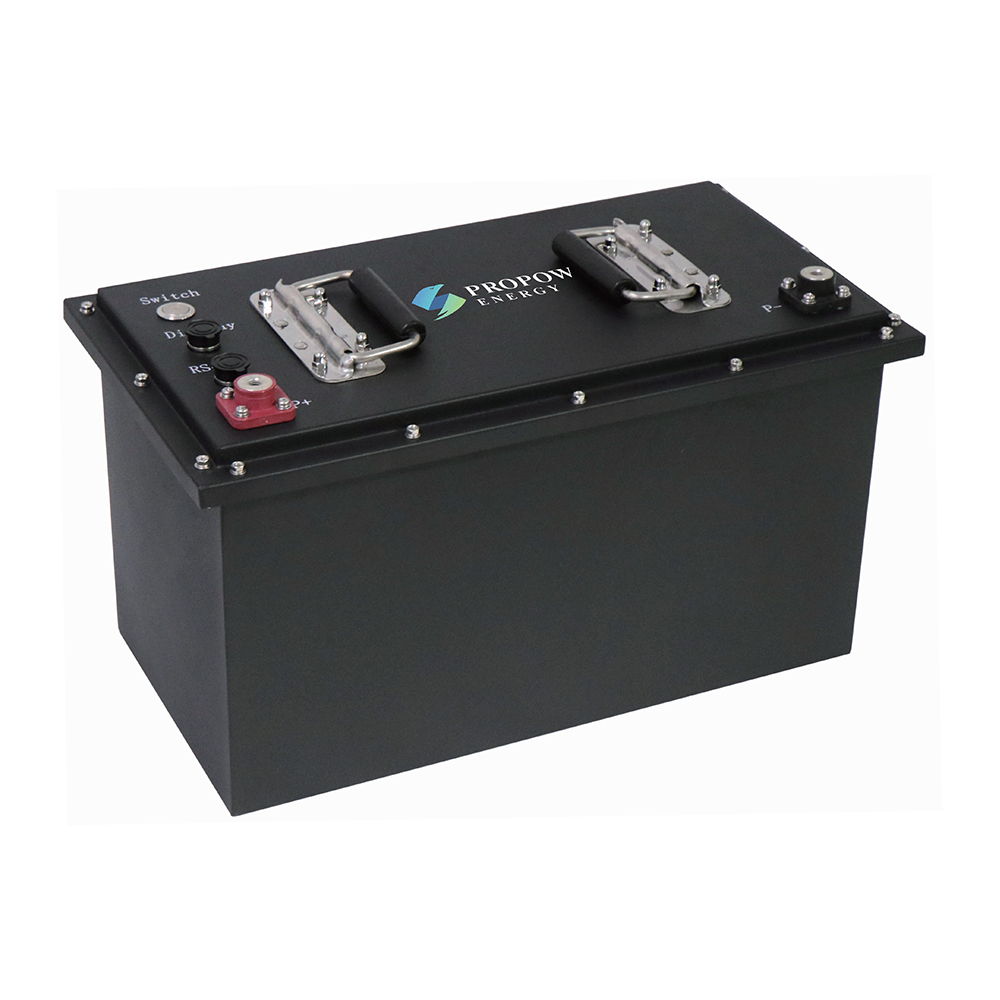 Aerial Work Platform Lithium Batteries
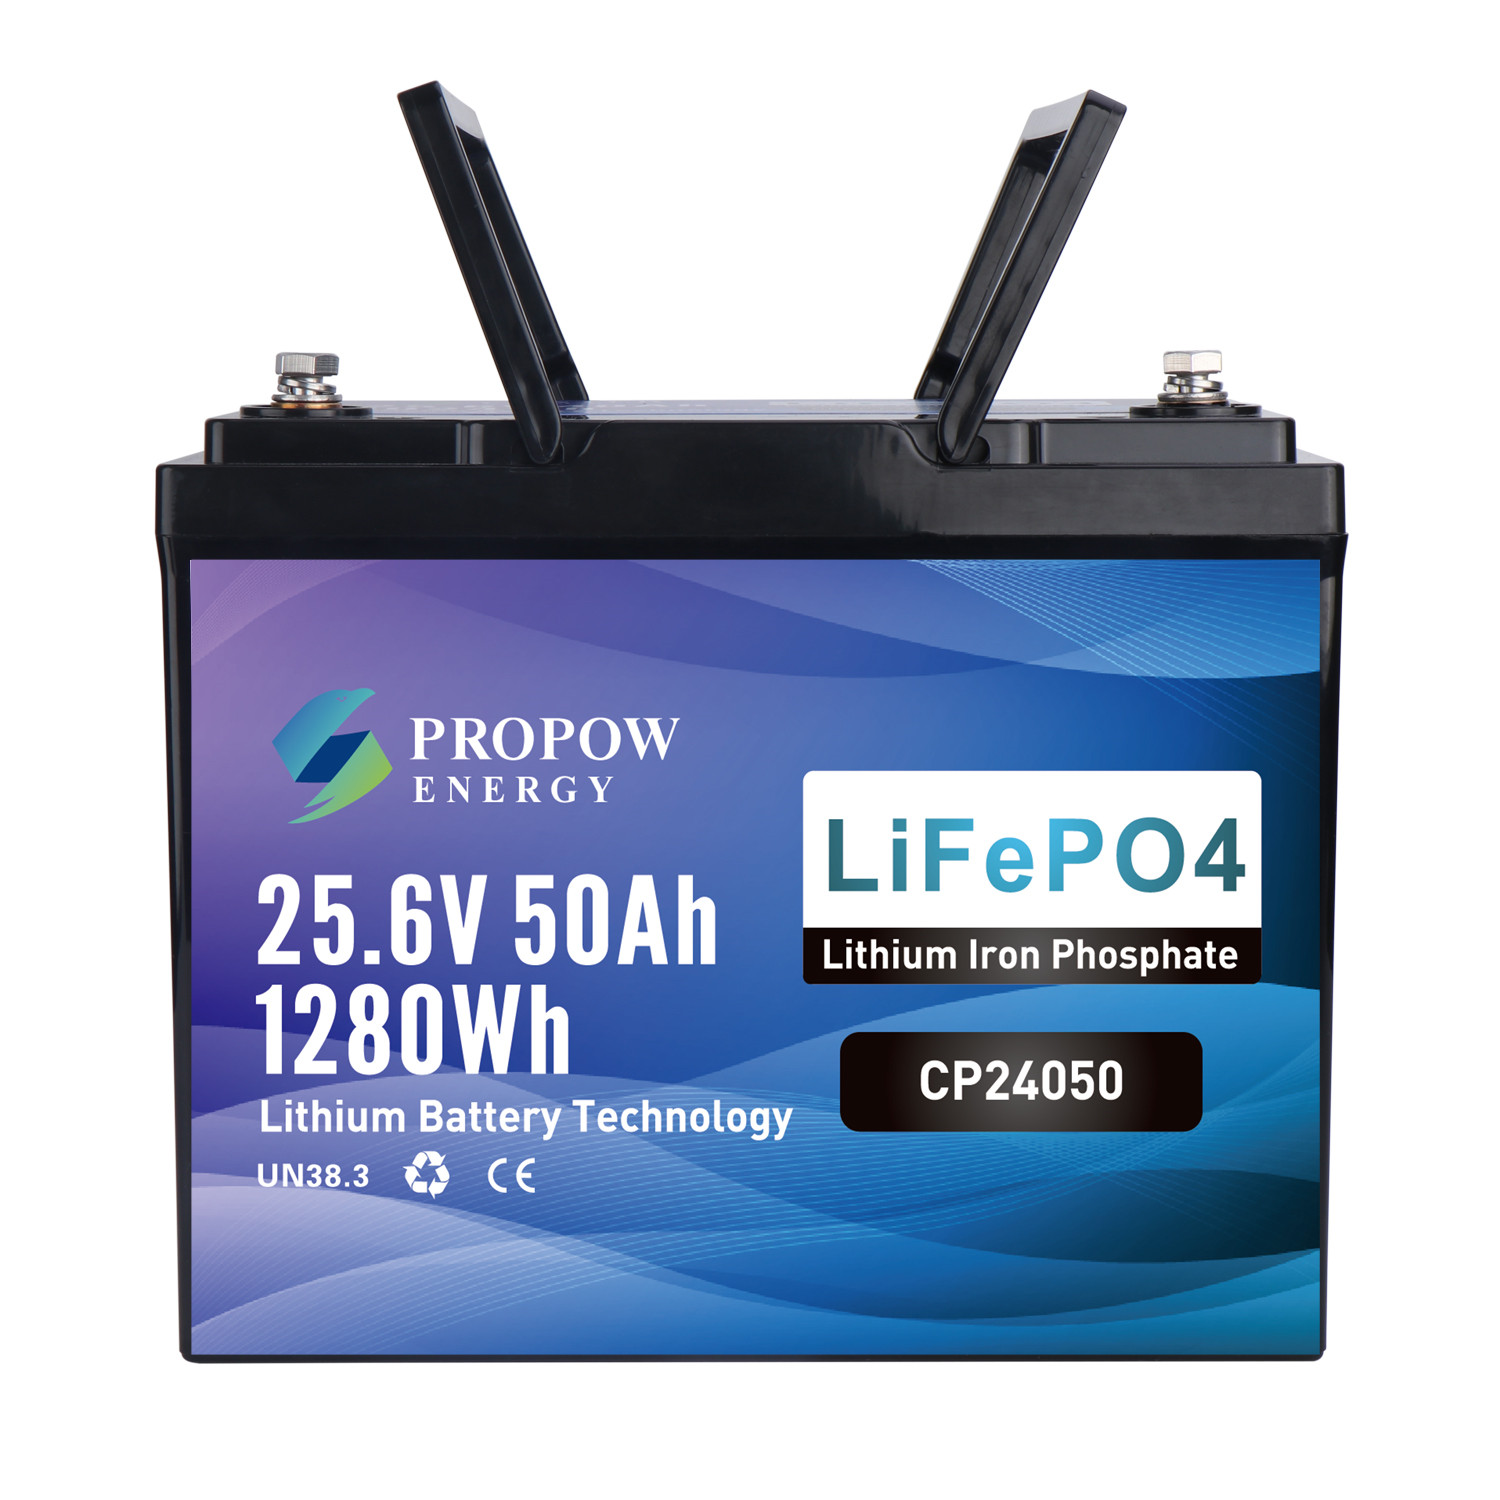 Industrial Automation Robot Batteries
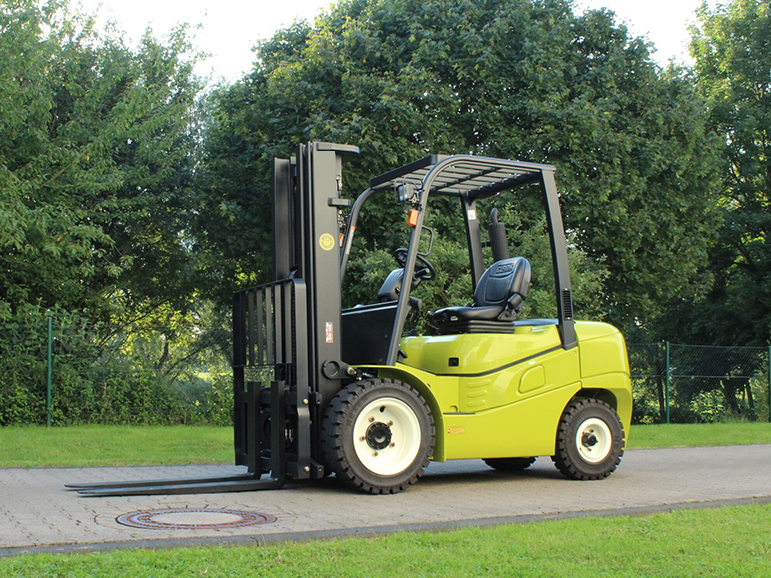 Electric Forklift Battery Solution
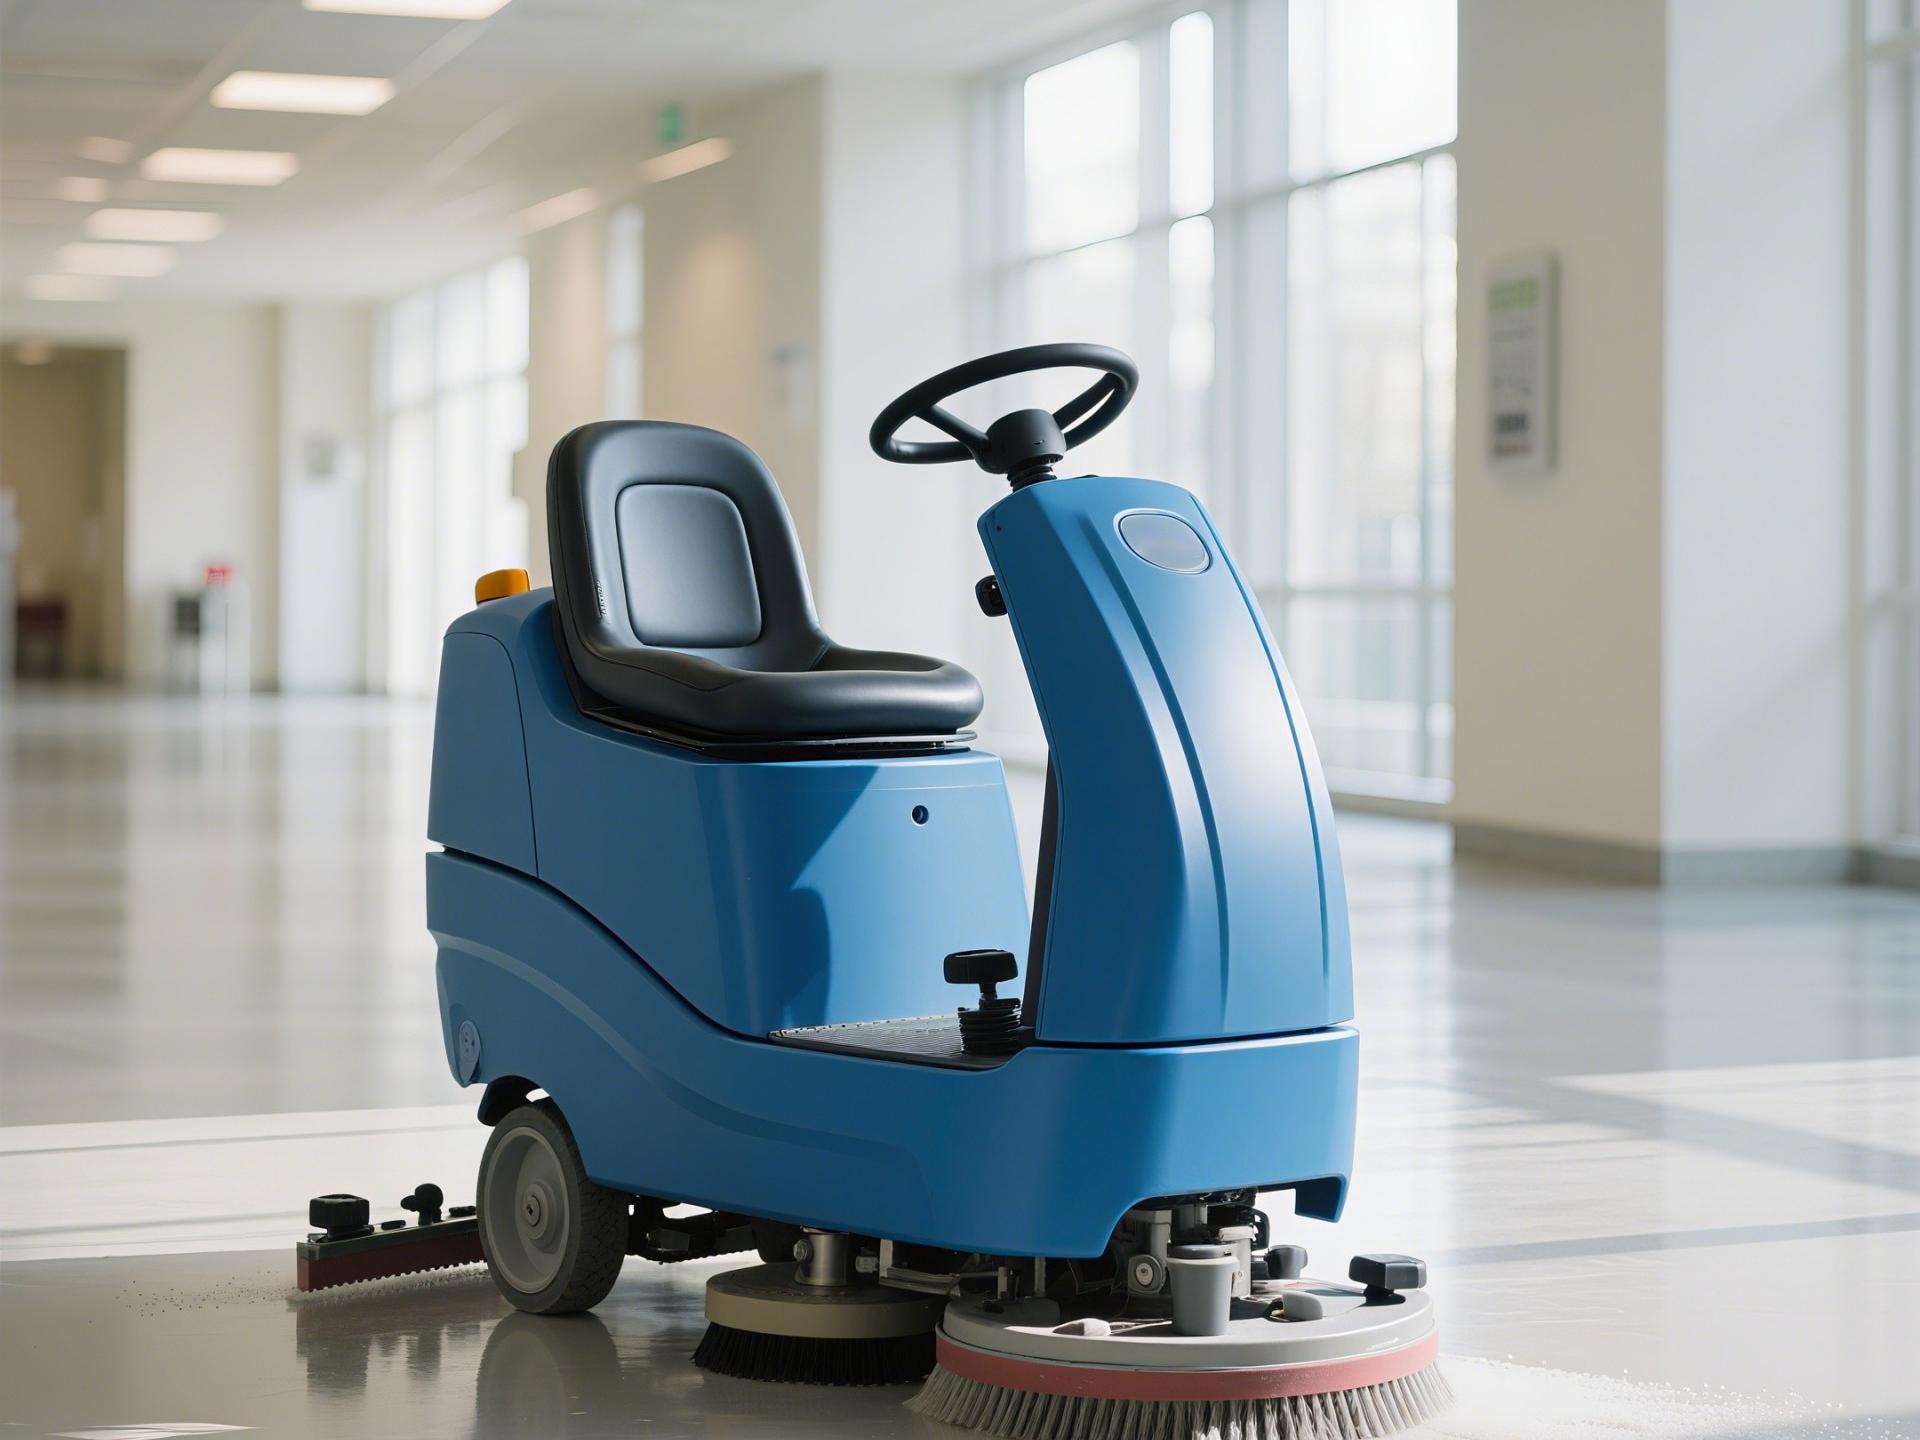 Floor Cleaning Machine Battery Solution
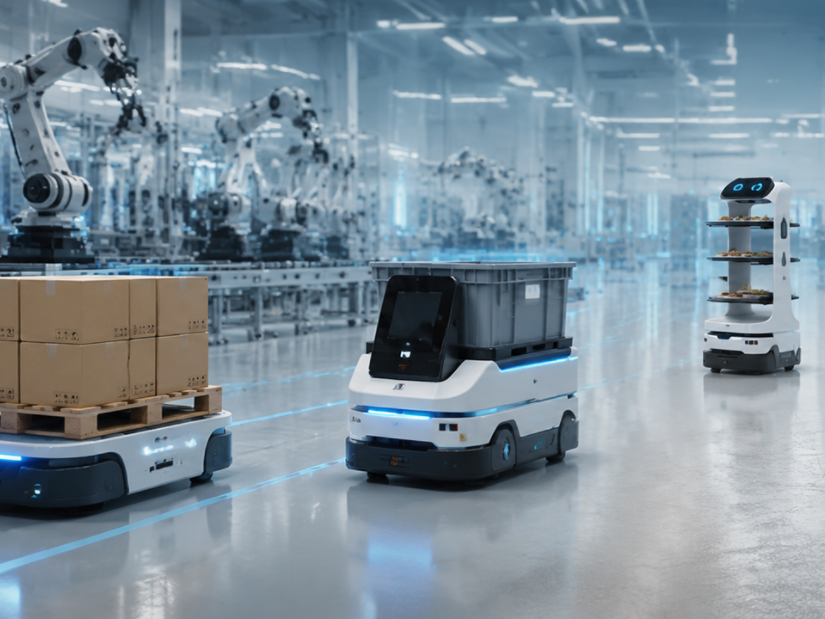 Industrial Automation Battery Solution
 Construction Equipment & Heavy-duty Trucks Solution
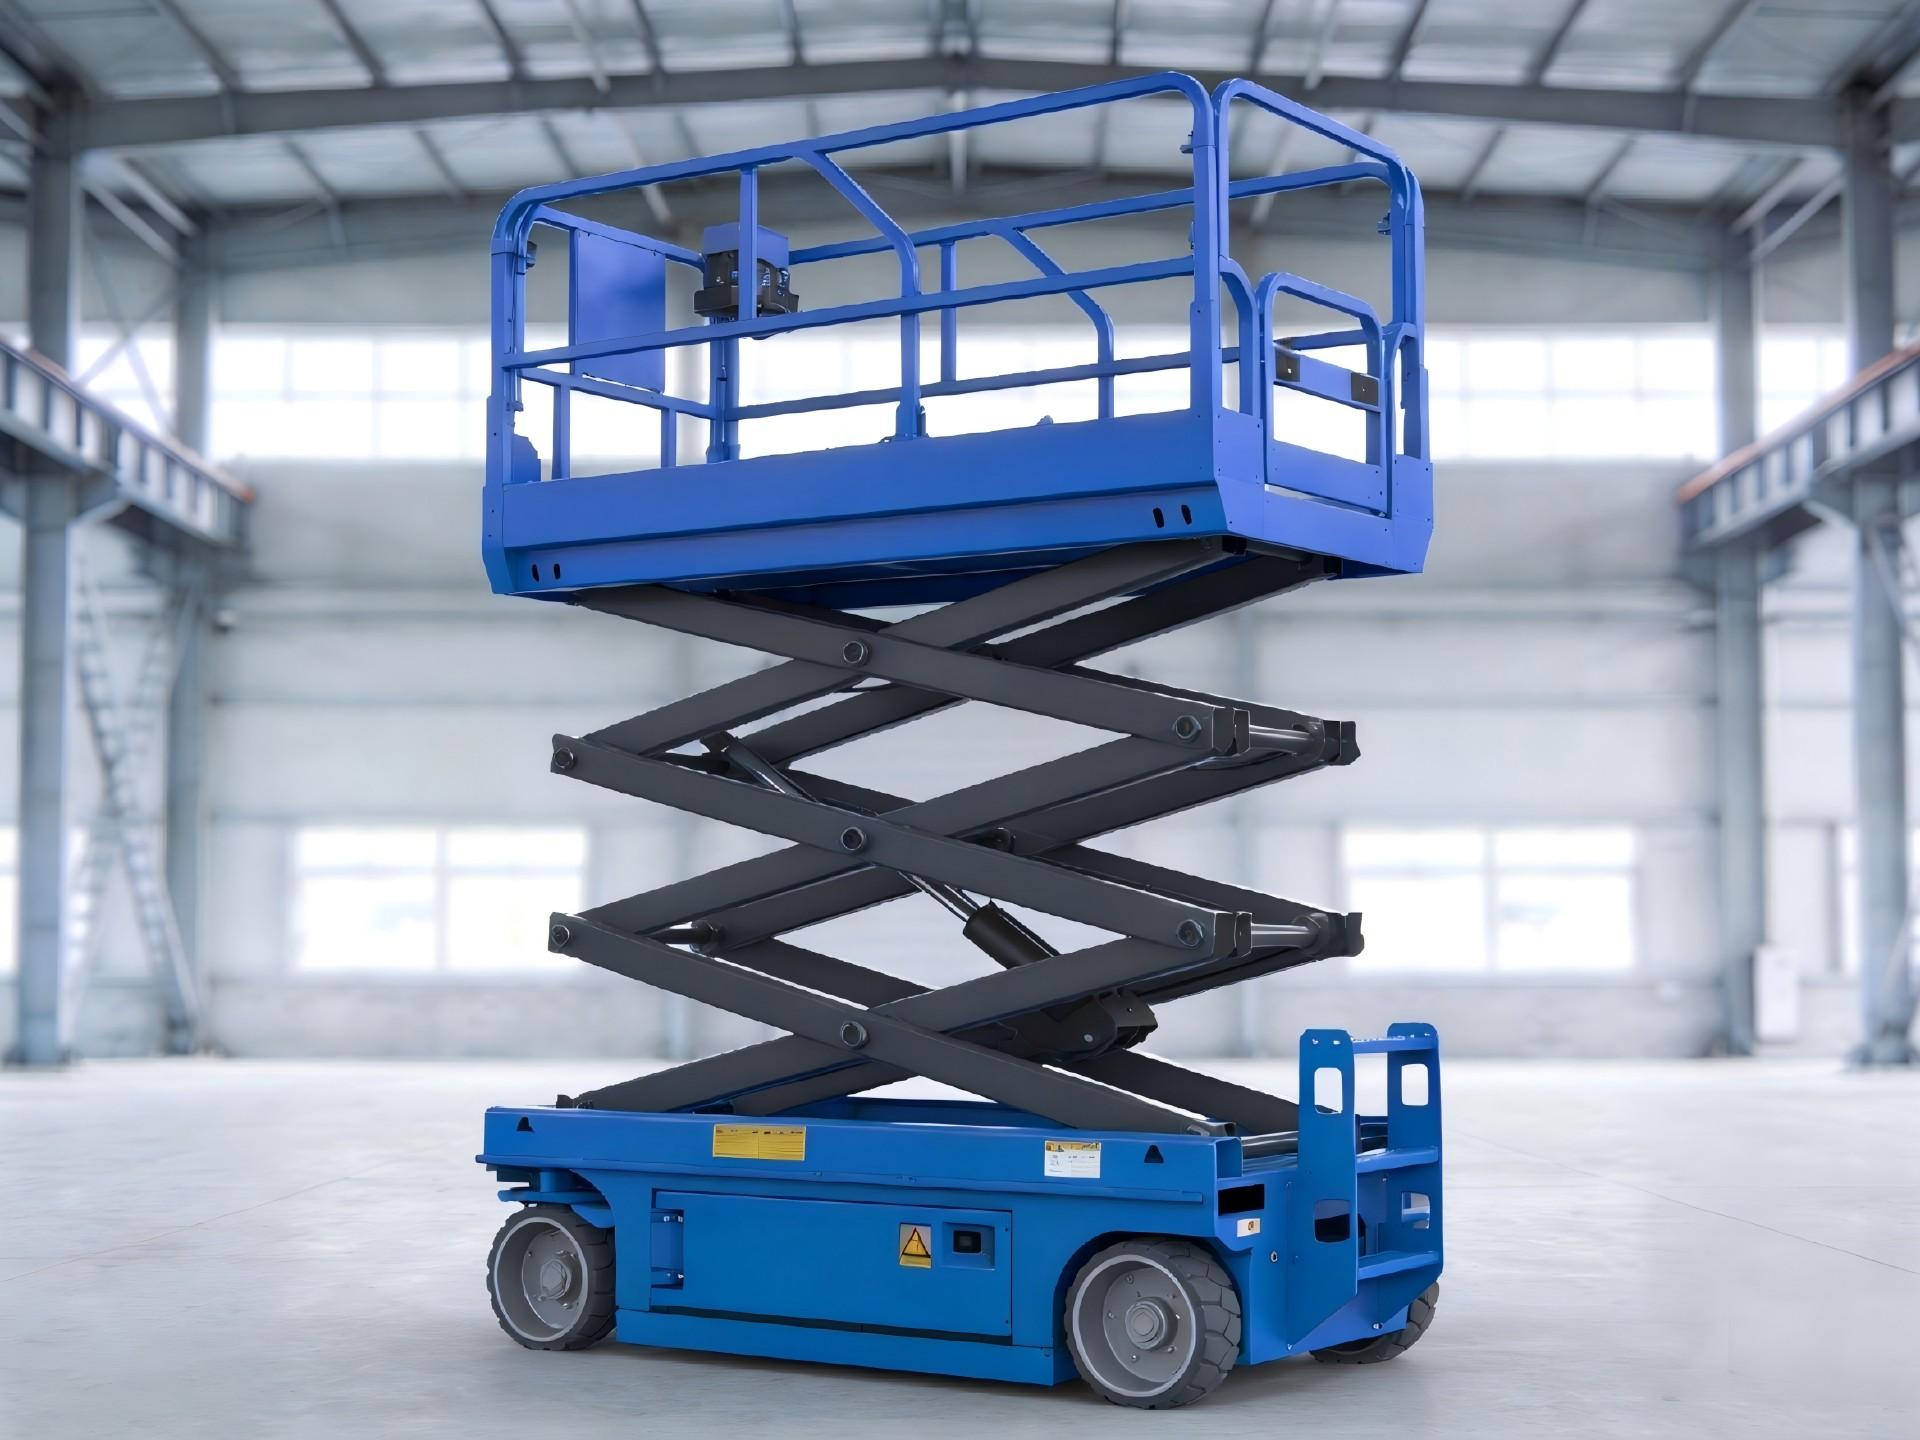 Aerial Work Platform Battery Solution
Leave Your Message
Heavy-duty power modules optimized for warehouse logistics, scrubbers, heavy equipment, and diamond processing support in Gaborone, Francistown, and Jwaneng.
A strategic analysis of motive power demands across Southern Africa's premier mining, trade logistics, and agricultural processing hubs.
As the economic powerhouse of the Southern African Development Community (SADC), Botswana has undertaken an aggressive modernization program across its mining infrastructure, dry port logistics terminals, and retail distribution centers. Material handling equipment—specifically electric forklifts, reach trucks, and heavy-duty counterbalance stackers—acts as the heartbeat of this commercial transformation. However, the harsh operating environments of the Kalahari basin, marked by blistering summer ambient temperatures exceeding 42°C, pervasive silica dust, and water conservation constraints, present demanding challenges for traditional motive power technologies.
Botswana's diamond mining giants (including operations around Jwaneng, Orapa, and Letlhakane) and coal reserves in Morupule require spark-free, zero-emission indoor and surface handling systems. Replacing legacy lead-acid batteries with hermetically sealed LiFePO4 traction packs eliminates corrosive acid fumes and explosion hazards in enclosed sorting rooms and mechanical stores.
The Gaborone Container Terminal (GABCON) and dry ports in Francistown serve as the multi-modal freight gateways for cross-border freight moving along the Trans-Kalahari Corridor and the North-South Rail link. Rapid 1-2 hour opportunity charging allows round-the-clock container yard operations without spare battery inventory.
The Botswana Meat Commission (BMC) in Lobatse and national beverage distributors require continuous operation in temperature-sensitive facilities ranging from deep-freeze storage (-25°C) to high-temperature distribution docks. Lithium traction batteries deliver constant voltage discharge without thermal shock failure.
For decades, companies in Botswana relied upon traditional lead-acid traction battery banks for their electric forklift fleets. However, operational audits consistently highlight severe vulnerabilities in regional deployment. Water scarcity is a critical reality across Botswana; lead-acid units consume hundreds of liters of demineralized distilled water monthly per forklift to replace electrolyte boil-off caused by ambient temperatures often rising above 38°C. Inadequate watering schedules result in rapid plate sulfation, acid stratification, and premature cell death within 14 to 20 months.
Furthermore, the open-vent charging of lead-acid packs releases corrosive hydrogen gas and sulfur aerosols. In Botswana’s dry, dusty climates, airborne particulate matter enters vented cells during routine maintenance, causing internal short circuits and accelerated degradation. Factory-built Lithium Iron Phosphate (LiFePO4) traction systems solve these problems completely. Featuring completely sealed IP65 or IP67 enclosures and active liquid/air thermal management, our industrial lithium packs prevent external contamination, eliminate daily maintenance labor, and endure extreme ambient thermal cycles with an operational lifespan exceeding 3,500 to 5,000 cycles.
Botswana benefits from an exceptional solar irradiation profile, averaging over 3,200 hours of sunshine per annum. Under the framework of the Botswana National Energy Policy and Vision 2036, commercial enterprises in Commerce Park (Gaborone), Dumela Industrial Area (Francistown), and Phakalane are rapidly installing rooftop solar photovoltaic arrays. LiFePO4 forklift traction batteries serve as ideal energy storage sinks: their high charge acceptance allows them to directly absorb peak midday solar power at high charge rates (0.5C to 1C), enabling warehouse operators to run material handling fleets on 100% clean, locally generated solar energy.
We are a leading manufacturer of high-performance lithium batteries for forklift, floor scrubber, aerial work platform, heavy-duty loader, and industrial automation equipment.
As a nationally certified high-tech enterprise, we integrate cutting-edge innovation with industry expertise. Our R&D team, drawn from top-tier companies like EVE, BYD, and CATL, helps us stay ahead of the curve. With over 109 patents and a commitment to international safety and transportation standards, we ensure the utmost reliability in every product.
We specialize in providing customized, dependable battery solutions for all your industrial needs in Botswana and international territories.



Our battery architectures integrate seamlessly with the world’s leading industrial equipment and cell manufacturers, offering direct drop-in replacement across Botswana’s leading forklift brands.
From underground diamond mining stores to bustling logistics distribution corridors in Gaborone and Francistown, explore our proven battery systems.
We provide full-spectrum customization services for industrial battery systems, covering design, voltage, capacity, size, and intelligent BMS integration to meet diverse application requirements across Botswana and Southern Africa. Backed by strong R&D and manufacturing capabilities, we ensure fast response, reliable quality, and tailored solutions.
Flexible Customization. Reliable Manufacturing. High Performance.
Looking for a Tailored Battery System? Get a Quote
Technical criteria for specifying LiFePO4 forklift motive batteries across British (BS) and European (DIN) counterbalance forklift chassis standard in Botswana.
In Botswana, material handling fleets feature a mix of Japanese, European, and South African sourced forklifts—most commonly Toyota, Linde, Jungheinrich, Komatsu, Hyster, and Nichiyu. Counterbalance electric forklifts demand precise counterweight tolerances; our custom steel battery boxes are laser-cut and ballasted to meet the exact minimum required weight ratings stated on your forklift data plate, preserving vehicle rollover stability and lifting capacity.
In central and western Botswana, ambient temperatures inside uninsulated metal warehouse facilities routinely top 45°C in the summer months. Our lithium traction batteries incorporate automotive-grade prismatic cells paired with an intelligent Battery Management System (BMS) with multi-point temperature sensors. If ambient heat spikes, the BMS dynamically adjusts continuous charge/discharge rates, preventing thermal runaway and protecting cell lifespan far beyond any lead-acid equivalent.
Managing forklift fleets distributed across remote locations like Francistown, Maun, and Palapye requires centralized oversight. Our lithium traction batteries feature integrated CAN-Bus 2.0B / RS485 communication protocols, interfacing directly with vehicle dashboards or cloud telematics. Fleet supervisors can monitor real-time State of Charge (SOC), State of Health (SOH), individual cell voltages, and charging events remotely.
Yes. Our engineering team builds custom ballast-weighted steel trays with exact dimensions and pin-out configurations to match Toyota, Jungheinrich, Linde, Komatsu, and other major brands. No structural forklift modifications are required.
Unlike lead-acid units requiring 8 hours of charging and 8 hours of cooling, our LiFePO4 batteries accept fast 1C charging. Operators can plug in during 15-minute tea breaks or 30-minute lunch shifts, eliminating the need for dedicated battery-changing rooms.
Our industrial LiFePO4 cells deliver over 3,500 full cycles at 80% Depth of Discharge (DOD). Backed by robust multi-year warranties, our battery packs offer 8 to 10 years of reliable service in Southern African environments.
We provide full export-compliant packaging under UN38.3, MSDS, and CE standards, facilitating smooth customs clearance via the Gaborone Dry Port (GABCON) or through transit corridors via Durban and Walvis Bay.
Explore all 8 high-performance industrial lithium batteries available for immediate factory order and customized engineering in the Botswana market.